SAE 52100

High-Carbon Chromium Steel For Bearing & High-Wear Applications

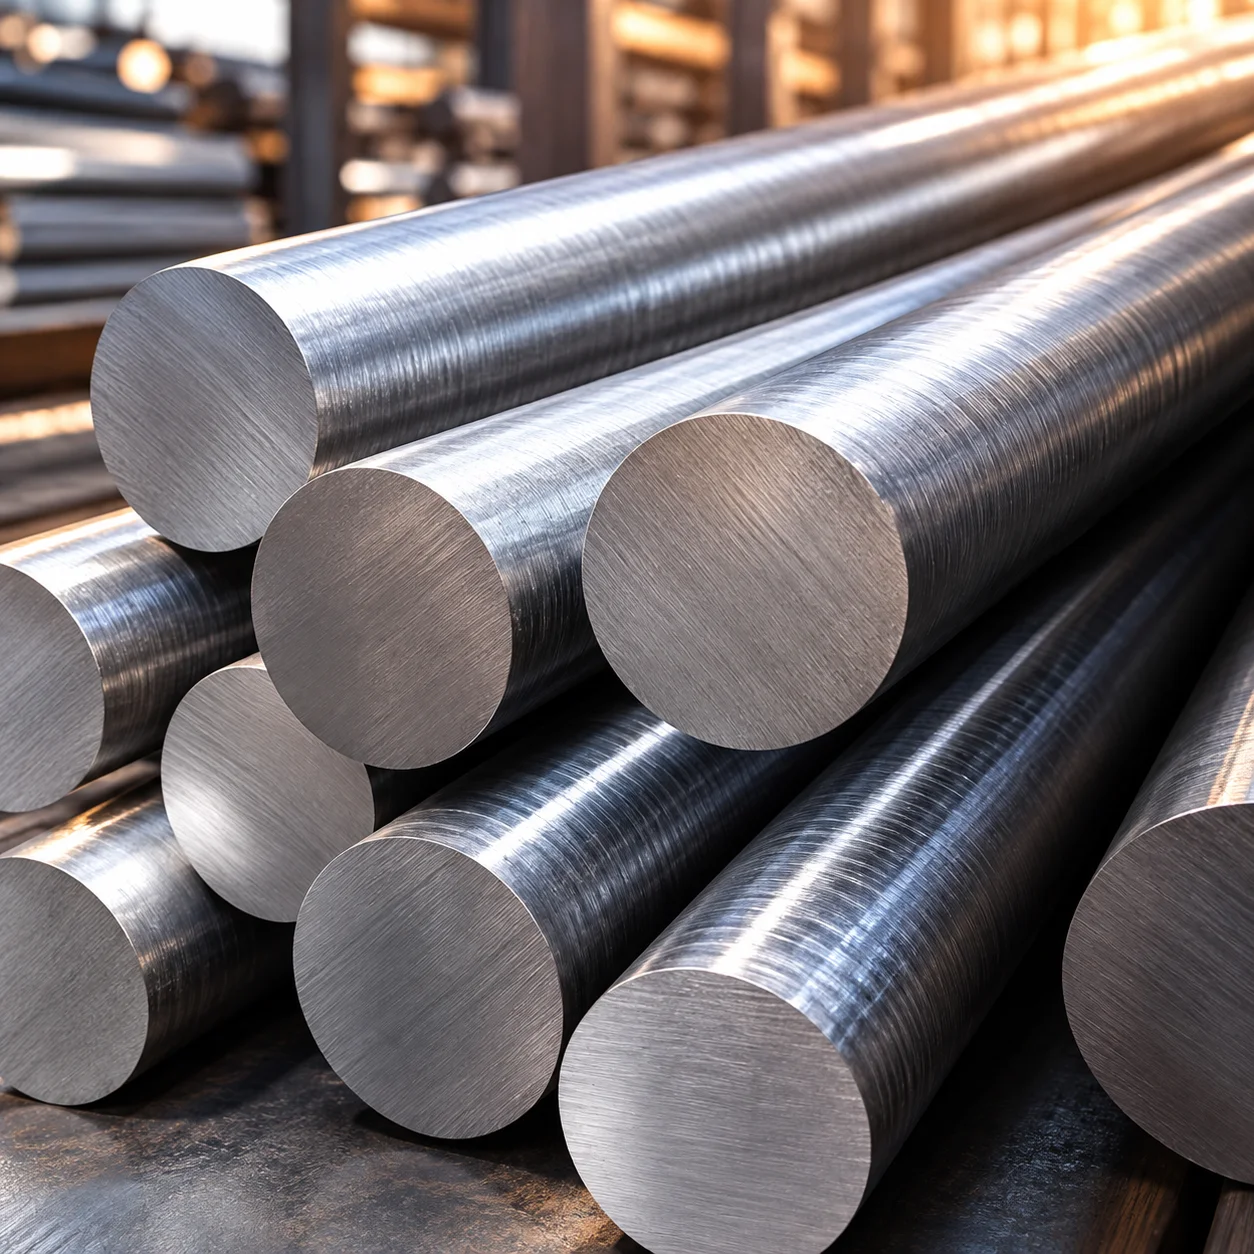
SAE 52100 is a high-carbon chromium alloy steel known for its high hardness, strength, wear resistance and fatigue performance. It is widely associated with bearing components and other precision machine parts exposed to repeated contact and high stresses.

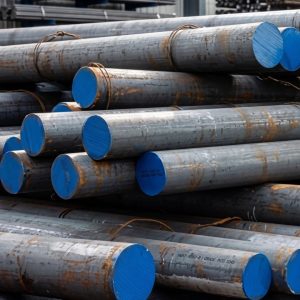
Available Forms: Round Bars, Blocks

Key Properties

  • High Hardness
  • Excellent Wear Resistance
  • High Fatigue Strength
  • Good Dimensional Stability
  • High Contact Strength
Category:

Technical Specifications

SAE 52100 — Technical Specifications 

Property Specification
Material SAE 52100
Steel Type High-Carbon Chromium Bearing Steel
Equivalent Designations 100Cr6, 1.3505, GCr15, SUJ2
Carbon (C) 0.98–1.10%*
Chromium (Cr) 1.30–1.60%*
Manganese (Mn) 0.25–0.45%*
Silicon (Si) 0.15–0.30%*
Phosphorus (P) ≤ 0.025%*
Sulphur (S) ≤ 0.025%*
Available Forms Round Bars, Flats, Blocks*
Supply Full Length / Cut-to-Size

Chemical Composition

Element Typical Range / Maximum
Carbon (C) 0.98–1.10%
Chromium (Cr) 1.30–1.60%
Manganese (Mn) 0.25–0.45%
Silicon (Si) 0.15–0.30%
Phosphorus (P) ≤ 0.025%
Sulphur (S) ≤ 0.025%
Iron (Fe) Balance


Applications

Where Sae 52100 Is Used

Bearing Components
Designed For Rolling-contact Applications Requiring High Hardness And Fatigue Resistance.

Rollers & Races
Suitable For Precision Components Exposed To Repeated Contact Stresses.

Balls & Rolling Elements
Used In Bearing And Precision Mechanical Applications.

Bushes & Sleeves
Suitable For Selected High-wear Mechanical Components.

Precision Machine Components
Used Where High Hardness, Strength And Wear Resistance Are Required.

High-wear Components
Suitable For Components Exposed To Repeated Mechanical Contact And Demanding Operating Conditions.

Heat Treatment

Heat Treatment For Performance

SAE 52100 is a through-hardening bearing steel. Heat treatment is used to develop the high hardness and strength required for bearing and high-wear applications.

Spheroidize Annealing

Typical cycle: RT → 820°C → controlled cooling

Used to develop a suitable microstructure for machining and subsequent hardening.

Hardening

Typical austenitizing range: 830–870°C

Followed by oil quenching for martensitic hardening.

Tempering

Typical range: 160–500°C

Tempering follows hardening to adjust the final hardness/toughness balance.

Stress Relieving

Typical range: 550–650°C

Can be used where stress relief is required before subsequent processing.

Available Forms

Available To Match Your Requirements

Round Bars — Precision steel for bearings, rollers and shafts.
Tubes — Suitable for specialised engineering applications.
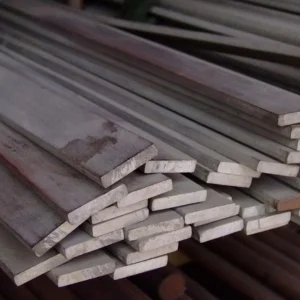
Flats — Designed for machining and industrial component requirements.

Supply Condition

Supply Conditions

SAE 52100 Can Be Supplied In Different Conditions Depending On The Customer’s Machining And Application Requirements.

Annealed

Suitable Where Improved Machinability Is Required Before Final Heat Treatment.

Spheroidized Annealed

Suitable For Machining And Preparation Before Hardening.

Hardened & Tempered

For Applications Requiring Developed Hardness And Mechanical Performance.

Full Length

Available According To Tsi Metals’ Stock Dimensions.

Cut-to-size

Material Can Be Prepared According To Customer-specified Dimensions, Subject To Availability.

Ovako’s 100cr6 Data Specifically Identifies Spheroidized Annealed, Quenched/Tempered And Tempered Conditions Among Its Heat-treatment Routes.